Why Choose a Triangular Screen for Industrial Screening?
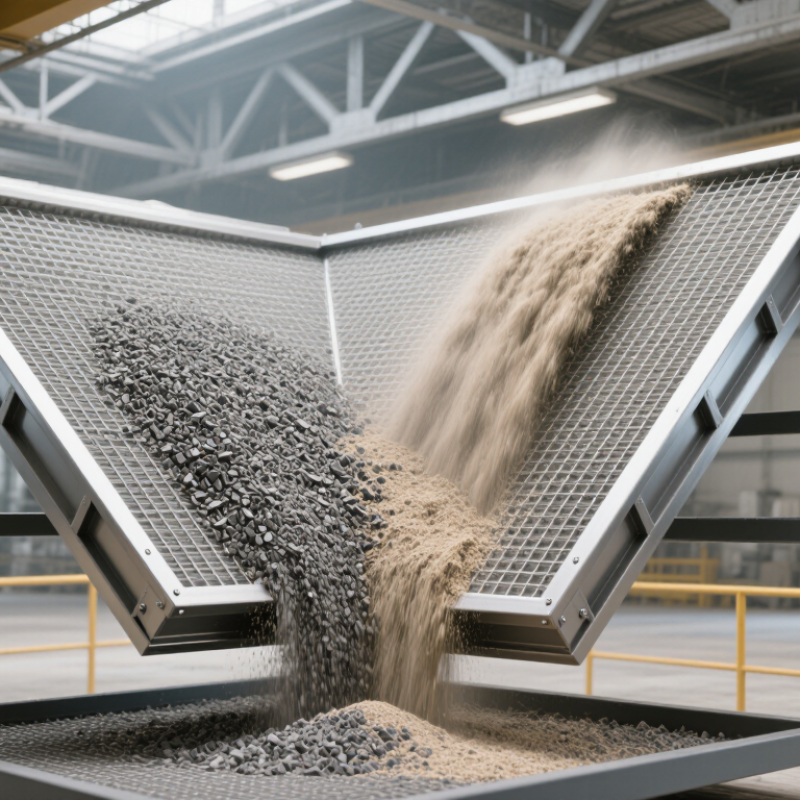
A Triangular Screen can make industrial screening more controlled when material needs steady movement across the deck. Its angled geometry helps guide particles while supporting separation by size. In a plant, that difference can show up in cleaner product streams, fewer misplaced particles, and a more predictable feed to the next process. But shape alone does not guarantee better performance. Aperture size, material moisture, feed rate, and screen maintenance all matter.
For transparency, no source article or verifiable expert quotation was provided, so a quotation should not be attributed to a real specialist. An illustrative line from a fictional screening engineer, Alex Morgan, captures the practical question: “Choose the screen for the material’s behavior, not for its shape alone.” Treat that as a prompt, not a sourced industry statement. The choice deserves a closer look. A Triangular Screen may suit applications where particle movement and separation consistency are priorities, yet it can be a poor fit if operating conditions are ignored. Even a well-designed unit can disappoint when blinded apertures or uneven loading go unnoticed. The following discussion examines how triangular geometry works, where it may help, and which operating details deserve careful evaluation before installation.
Triangular Screen Fundamentals: Profile-Wire Geometry and Slot Dimensions
A triangular profile wire has a narrow surface opening and a wider channel beneath it. This tapered geometry lets near-size particles pass with less wedging than a parallel-sided slot. Small details matter. Slot width is measured at the screening face, while wire pitch is the distance from one wire to the next. For parallel slots, the approximate open-area ratio is slot width divided by pitch. Wider slots can raise capacity, but may also let unwanted particles through.
The USGS Mineral Commodity Summaries 2024 estimated U.S. crushed-stone output at about 1.5 billion tons in 2023; its estimated construction sand and gravel output was about 1 billion tons. These figures show the scale of screening demand, not a universal slot specification. In practice, measure the feed’s particle-size distribution, then compare the target cut size with the narrow slot opening. Check wire height and support spacing too: a thin wire may offer more open area, yet flex or wear faster under heavy loads. There is a trade-off. Dust, moisture, and irregular particles can change performance, so a clean-water test may mislead. Pilot results are useful, but never perfect.
Aperture Selection: ISO 565 Nominal Sizes from 20 µm to 125 mm
Why Choose a Triangular Screen for Industrial Screening?
Aperture Selection: ISO 565 Nominal Sizes from 20 µm to 125 mm
Choosing an aperture begins with the particle size you need to retain or pass. ISO 565:1990 lists preferred nominal sieve openings from 20 µm to 125 mm. This gives engineers a shared sizing reference, rather than an improvised mix of labels. Start with the target cut, then check nearby standard sizes against the material’s real particle distribution. Small changes matter. A few micrometres can shift fine-powder yield; a wider opening can let coarse fragments through.
Triangular openings can offer useful flow paths, but nominal size alone does not predict separation performance. ISO 565 defines aperture sizes, not a guaranteed cut point for every screen geometry. Particle shape, moisture, bed depth, and screen loading also affect passage. ISO 3310-1:2016 sets requirements for test sieves made from metal wire cloth, offering a reference for aperture verification. For triangular screens, confirm how the clear opening is measured and request inspection data. On paper, this is neat. In a wet plant, it is not. A quick trial with representative feed can expose blinding or unexpected carry-over before a full installation.
Capacity Drivers: Open Area, Feed Rate, and Particle-Size Distribution
Capacity depends on more than a triangular screen’s dimensions. Effective open area determines how much material can pass through at once, while the screen’s profile and slot arrangement influence separation. A higher open-area ratio may increase throughput, but it can also reduce the support available to the material. Small details matter. Check the usable openings, not just the panel’s outside measurements.
Feed rate needs to match the screen’s working area. A steady, even layer gives particles more chances to contact an opening; a deep surge can bury the surface and slow separation. In practice, watch where material builds up and whether the discharge stays consistent. That can mislead. A short test at the actual feed rate may reveal problems that a capacity estimate misses.
Particle-size distribution is just as important. If most particles are close to the cut size, passage may be slower than it is with a broad mix of clearly small and clearly large particles. Fine, damp material can also cling or blind openings, even when the nominal open area looks generous. Record the feed’s size range and moisture, then compare them with the required cut. Still, calculations have limits; actual material often behaves less neatly than a sample report suggests.
Why Choose a Triangular Screen for Industrial Screening?
Capacity Drivers: Open Area, Feed Rate, and Particle-Size Distribution
Illustrative dry-screening cases for an 8 mm cut size. Actual capacity depends on material properties, screen motion, deck dimensions, and operating conditions. | Operating case | Triangular-slot screen | Open area | Feed particle-size distribution | Feed rate | Indicative screening result |
| Moderate loading | 8 mm nominal slot; triangular profile wires | 35% | 60% below 6 mm; 15% from 6–10 mm; 25% above 10 mm | 3.0 t/h per m² of active deck | About 96% of undersize material passing the deck |
| Balanced feed | 8 mm nominal slot; triangular profile wires | 40% | 70% below 6 mm; 20% from 6–10 mm; 10% above 10 mm | 5.0 t/h per m² of active deck | About 93% of undersize material passing the deck |
| High near-size content | 8 mm nominal slot; triangular profile wires | 40% | 55% below 6 mm; 35% from 6–10 mm; 10% above 10 mm | 4.0 t/h per m² of active deck | About 86% of undersize material passing the deck |
| Higher open area and loading | 8 mm nominal slot; triangular profile wires | 45% | 70% below 6 mm; 20% from 6–10 mm; 10% above 10 mm | 7.0 t/h per m² of active deck | About 88% of undersize material passing the deck |
Particle-size bands are defined relative to the 8 mm cut: undersize is below 6 mm, near-size is 6–10 mm, and oversize is above 10 mm. The figures are representative examples for comparison, not guaranteed equipment ratings.
Performance Checks: Evaluate Screen Efficiency, Blinding, and Wear rate
A triangular screen uses wedge-shaped openings that widen beneath the screening surface. This geometry can help particles pass through and reduce wedging, but it does not guarantee higher efficiency. Check performance with a representative feed sample. Record feed rate, particle-size distribution, and the amount of misplaced material in both product streams. Compare results under consistent operating conditions; otherwise, changes may reflect the feed rather than the screen.
Blinding can develop when damp fines or near-size particles lodge in the openings. Inspect several areas, not just the center, and note blocked apertures after a defined run time. Wear also deserves regular measurement. Compare wire thickness and opening dimensions at high-impact zones with less-used areas. A clean-looking panel can still have enlarged openings. Small details matter. One limitation is that manual checks can miss gradual changes, especially when inspections are irregular.
Tips: Keep a simple log of efficiency, blocked openings, and wear measurements. Photograph the same screen locations each inspection. If blinding rises, check moisture and feed consistency before changing the screen. Small trials help separate screen effects from operating changes.